Manufacturing Process of Luggage Hardware Hooks and Buckles: A Journey of Precision from Raw Materials to Finished Products
Hook and buckle fittings are core functional hardware for handbags and luggage. Seemingly simple finished items go through multi‑stage precision manufacturing procedures starting from molten metal raw‑material.
This article breaks down six core production phases: die‑casting, spring‑&‑pin component preparation, assembly, polishing‑deburring, electroplating and final quality‑inspection, delivering process‑reference for leather‑goods procurement and quality‑control teams.
Materials Science & Mould Engineering for Luggage Hardware Casting
Precision manufacturing begins with meticulous control over materials and moulds. Just as a building requires a solid foundation, so too are the durability and texture of snap fasteners established in this way.
Alloy Material Selection for Snap Hook & Buckle Fittings
Not all metal alloys are suitable for manufacturing snap hooks and buckle hardware for handbags and luggage. Zinc alloy is the most widely adopted option thanks to its excellent fluidity when molten, which supports intricate mould filling during die casting. Brass delivers superior strength and corrosion resistance for high-end custom hardware, while iron hardware serves cost-sensitive applications with limited decorative finish requirements.
When selecting raw alloy materials, our engineering team evaluates key indicators including melt temperature, tensile strength, ductility and plating compatibility. A well-chosen alloy avoids casting defects such as shrinkage cavities and poor surface coverage during later electroplating.
Precision Mold Design for Cast Hardware Blanks
Mould quality is the foundation of consistent hardware blanks. All mould cavities for snap hooks and buckles are CNC machined from high-quality tool steel. Engineers design gate positions, parting lines and ejection structures according to the hardware shape.
Well-designed moulds reduce flash and parting-line burrs on cast blanks. This lowers the workload for subsequent polishing and deburring, stabilises batch consistency and minimises surface flaws that would show up after electroplating.
Once the alloy material formula is confirmed and the precision casting mould is finished, we proceed to the die casting stage to form hardware blanks.
Phase 1: Die‑Casting — Forming Raw‑Material Hardware Blanks
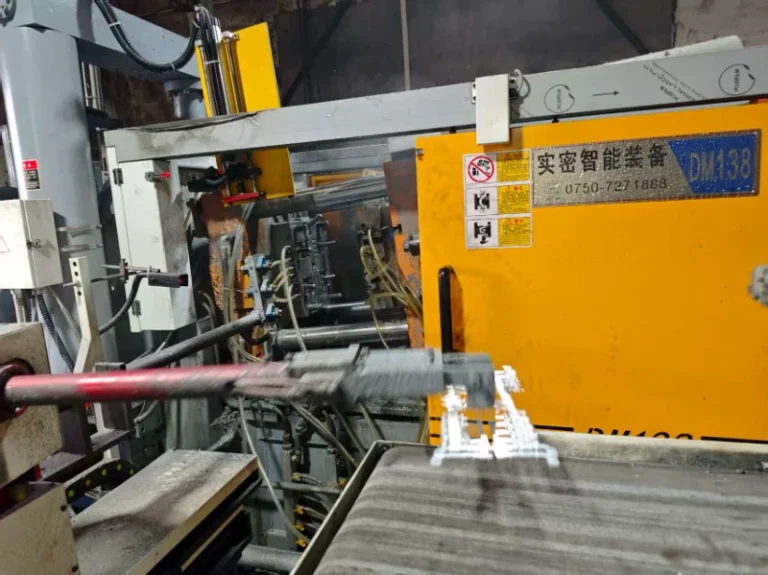
Die casting is the foundational process that gives the hook its basic shape, determining its inherent quality and initial contour.
- Raw‑Material Melting: Zinc‑alloy or copper‑alloy ingots are heated inside furnaces to molten state at 400‑500 °C for die‑casting filling.
- Mould Precision: Mould cavities are CNC‑machined from high‑grade tool steel with mirror‑polished interior surfaces, securing consistent geometry for high‑volume batches.
- High‑Pressure Injection & Solidification: Molten alloy is injected at high‑speed high‑pressure into mould cavities, rapidly cooling under pressure to produce solid hardware blanks.
- Core Quality Control: Strict temperature‑&‑pressure control is required to achieve dense internal structure without voids; this forms the first quality barrier for tensile‑load and repeated opening‑closing performance
Phase 2: Spring & Pivot‑Pin Component Preparation
Springs and pins form the functional core of the snap‑hook., directly determining its opening and closing feel, smoothness, and service life.
Torsion‑Springs: Core Of Opening‑Closing Function
High‑quality stainless‑steel torsion‑springs must sustain tens‑of‑thousands of open‑close fatigue cycles, maintaining stable elastic force across the hardware service‑life.
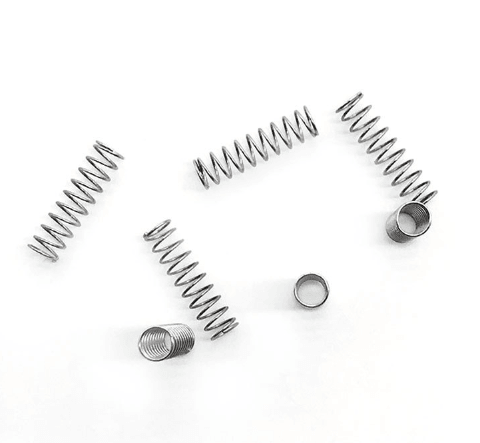
Pivot‑Pins: Rotating Connection Components
We strictly control the size error of the pins within an extremely small range to ensure flexible and safe integration with the hook body’s hole diameter.
- Precision dimensional tolerance control: Pin dimension error must be tightly controlled to achieve smooth fit inside hook‑body holes with minimal play or wobble.
- Surface hardening‑carburizing treatment for pins creates hard wear‑resistant outer layer while retaining inner‑material toughness. This “hard‑outside, tough‑inside” property lowers bending‑and‑fracture risk during repeated use.
Phase 3: Component Assembly Into Functional Hardware Units
Assembly integrates die‑cast blanks, springs and pivot‑pins into complete working buckle /snap‑hook units, balancing production‑efficiency and assembly‑precision.
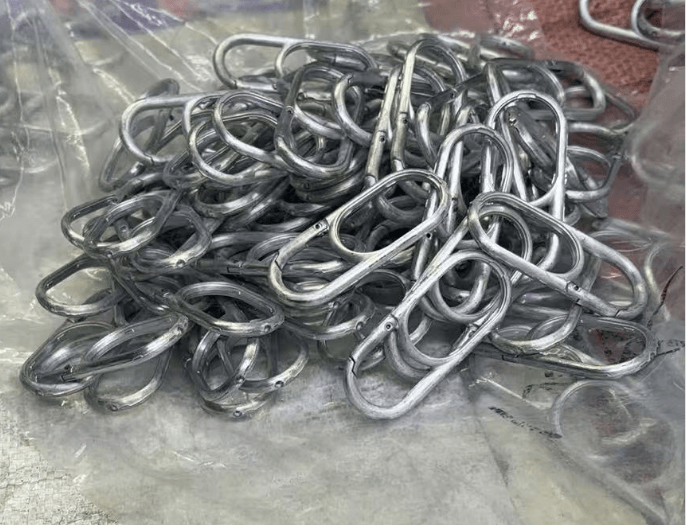
- Automated workflow: Vibratory feeders and robotic‑arm equipment are widely deployed for high‑volume batches to press‑fit springs and pins. Real‑time monitoring of pressing‑pressure and positioning guarantees batch‑consistency.
- Manual assembly for complex /high‑end hardware: Experienced technicians complete assembly for intricate premium‑grade hardware where automated equipment cannot handle fine complex details.
Phase 4: Polishing & Deburring — Surface Pre‑Treatment Before Electroplating
This process eliminates the rough surfaces and burrs produced by die-casting and mechanical processing, creating the perfect raw material for the subsequent electroplating
Mass‑Barrel Polishing Process
Hardware blanks are loaded inside polishing barrels together with abrasive media. Extended mechanical friction removes surface oxidation, casting‑scratches and surface imperfections, delivering uniform matte or pre‑gloss surface condition ready for plating.
Deburring: Removing Parting‑Lines & Sharp Flash
- Traditional workflow: Manual removal of mould parting‑lines and sharp flash by files and abrasive paper.
- Modern high‑efficiency workflow: Electrolytic deburring or magnetic‑grinding. Magnetic‑grinding uses magnetic‑field‑driven stainless‑steel media to clean complex crevices and inner‑hole dead corners thoroughly
Electroplating: The Final Barrier and Finishing Touch
The final step – electroplating, gives a hook and ring fastener a fine shiny look, making it not only visually appealing, but strong and resistant, as well. In this way, we combine aesthetic features with the necessary protective properties.
Functional & Aims Of Electroplating Treatment
- Corrosion‑resistance & wear‑resistance: Form compact metal coating to defend base‑alloy from oxidation, rust and daily‑use abrasion.
- Decorative styling: Achieve diverse metal finishes such as nickel, gold, gun‑metal black matching different luggage‑design requirements.
Electroplating Production‑Procedure Requirements
Hardware parts act as cathode inside electrolyte solution containing target‑metal ions. Operators precisely control current density, bath‑temperature and processing‑time to deposit even‑thickness plating layers. Special finishes such as matte‑black may require supplementary post‑plating spray‑coating to prevent discoloration.
Poor surface condition from upstream die‑casting / polishing defects will become more visible after plating. Electroplating quality serves as final validation indicator for all preceding manufacturing steps
Phase 6: Final‑Batch Quality‑Control & Export‑Grade Packaging
H3|Multi‑Dimension Finished‑Goods Inspection
- Visual check: surface finish, plating continuity, scratch / blemish screening
- Functional test: spring‑gate opening‑closing smoothness & spring‑tension retention
- Dimensional verification: critical dimension conformance against drawing
- Sampling mechanical test: partial batch sampling for tensile‑load and salt‑spray corrosion‑testing
Anti‑Scratch Export‑Grade Packaging
Qualified hardware components are individually protected before carton‑packing to avoid surface‑scratch damage during transit.
FAQ for Luggage‑Hook & Buckle Manufacturing
Q1: What are the most‑common hidden defects originating in die‑casting phase?
A: Internal voids / porosity, insufficient material filling, gate‑flash. Those invisible inner defects may lead to hardware fracture under load even if surface looks perfect.
Q2: Why do perfectly‑plated buckles still have poor spring‑gate hand‑feel?
A: Problems usually root in spring‑material grade, pin‑dimensional tolerance or assembly pressing‑parameters; surface plating cannot fix mechanical‑assembly defects.
Q3: What risks will happen if skipping thorough deburring before electroplating?
A: Remaining sharp flash and parting‑lines will keep existing after plating; burrs may scratch webbing, leather or end‑user skin.
Q4: Can electroplating compensate bad quality from polishing and die‑casting?
A: No. Electroplating is a thin surface‑coating; underlying casting‑scratches and surface imperfections will still show after plating. Up‑stream quality control cannot be replaced by post‑plating.
Q5: What key test‑items should buyers require for finished hook‑buckle batches?
A: Visual‑surface inspection, opening‑closing functional check, key dimension measurement, spring‑fatigue cycle test, sampling tensile‑strength test and salt‑spray corrosion test.
Conclusion
Manufacturing for luggage‑hook and buckle hardware is a multi‑step precision industrial workflow: die‑casting creates the base blank; carefully‑selected springs and pivot‑pins deliver core mechanical‑function; assembly integrates discrete parts; polishing‑deburring prepares surface quality; electroplating provides corrosion‑resistance plus decorative finish; final quality‑control validates overall batch‑performance.
For B2B procurement teams: final hardware reliability depends not merely on finished‑sample appearance, but consistent parameter‑control across every preceding production phase. Buyers should define requirements for die‑casting density, spring‑fatigue cycles, plating‑thickness and QC‑sampling‑rules within technical specifications before mass‑production.
OYC Hardware supplies stock and custom‑mould hook‑and‑buckle luggage hardware and can provide corresponding mechanical‑test and corrosion‑resistance documentation for cross‑border bulk‑orders.
.Discuss Your Luggage‑Hardware Hook & Buckle Project
- Chat on WhatsApp +86-13924451472
- Submit Your Hardware Requirement