Avoid Sample‑to‑Bulk Discrepancies for Handbag Hardware | QC Guide | OYC Hardware
In the luggage‑goods industry, one of buyers’ biggest pain points is approved samples that do not match final bulk production. Color shifts, inconsistent texture, dimensional drift, and uneven spring tension are often only discovered when bag factories start assembly work. These issues cause delayed shipments and substantial rework costs. Many buyers assume such gaps are purely caused by suppliers cutting corners. In fact, sample‑bulk discrepancies mostly stem from details in prototyping, mold maintenance, electroplating and production hand‑over. As a professional hardware manufacturer, we break down these common root causes and share practical preventive measures.
Common Causes of Sample‑to‑Bulk Discrepancies
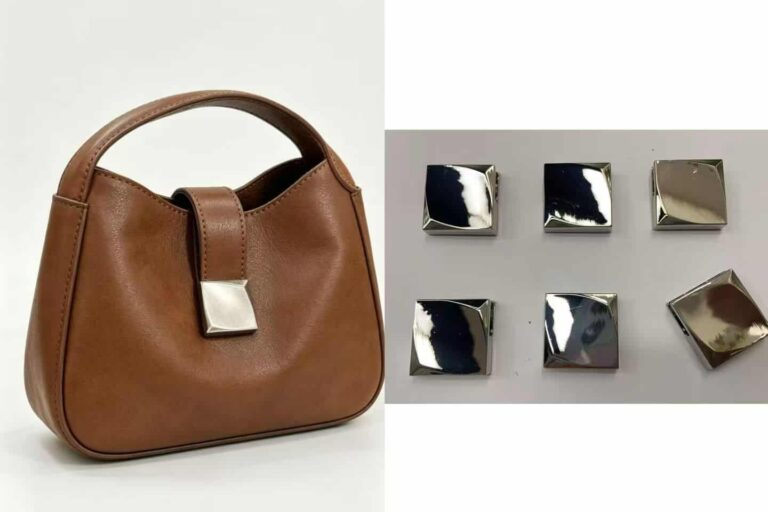
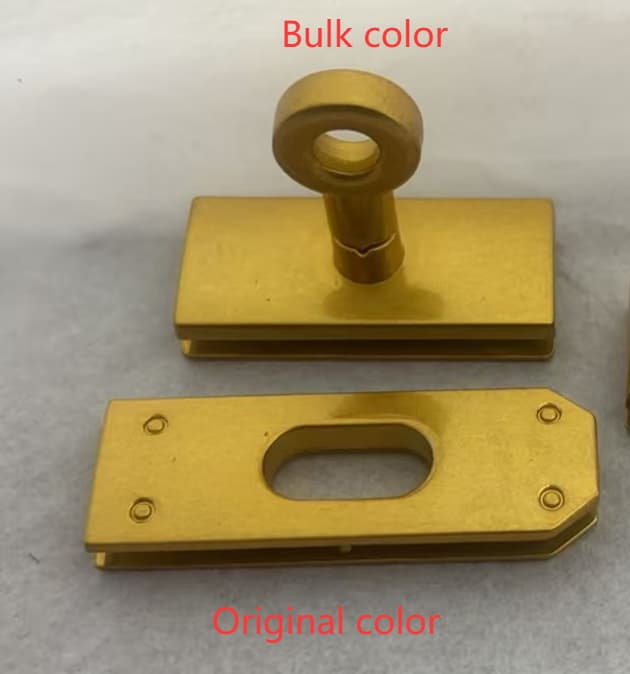
Plating Color: The Most Common Pitfall
Prototyping typically involves electroplating in small tanks. In small tanks, the concentration of the plating solution is stable, the number of samples is small, the immersion time is controllable, and it is easy to achieve a uniform and attractive color. However, during mass production, we do electroplating in large tanks in batches; as we continuously consume the plating solution, fluctuations in temperature and current can easily lead to color discrepancies
Many customers only keep a paper color chart and do not retain a physical confirmation sample.When we complete the mass production run, discrepancies arise because both parties use different criteria to judge color
Solution
The client must sign off on and seal the physical reference sample, while also retaining a standard color swatch. Before we begin mass production plating, we must create pre-production test pieces; we should only proceed with mass plating after the client has approved these test pieces. Throughout the entire mass production run, we must compare the finished products against the signed reference sample; we should not judge color based solely on photographs of the sample
For export orders, we also suggest defining acceptable color tolerance and referencing Pantone metal color codes alongside physical sealed samples.
Mold Issues: Dimensions, Curvature, and Hole Positions Have Quietly Deviated from Specifications
The prototyping phase often involves hand-made prototypes or simple test molds, which offer high precision but are not suitable for mass production. Once we replace these with steel production molds, the mold may wear and slightly deform after we have stamped it tens of thousands of times. This directly results in differences in metal thickness, bend radius, and hole spacing compared to the sample.
Another scenario is when, during prototyping, we intentionally refine and polish the mold to achieve an attractive appearance, but we simplify the polishing process for mass production, resulting in noticeable differences in edges, corners, and the feel of the product
Solution
After we complete the production mold, we first produce a pre-production sample and compare its dimensions, hole positions, and overall shape with the original approved sample.. Once everything has been verified and confirmed to be correct, proceed with mass production. Perform regular inspections and maintenance on the mold, and repair it promptly upon any signs of wear to prevent dimensional drift.
Hand‑polished prototype molds cannot be directly treated as mass‑production steel‑mold standards.
Materials and Components: Quietly Switching Raw Materials
When producing samples, factories typically select higher-quality raw materials. The cost of different grades of zinc alloy, iron, and stainless steel varies significantly. Some manufacturers switch to lower-grade materials during mass production, resulting in differences in the weight and hardness of the hardware. For example, samples may be thick, while mass-produced items are thinner; samples may be resistant to deformation, while mass-produced items bend even under light pressure.
There are also differences in the plating materials: samples have a thick sealing oil coating, providing excellent rust protection; mass-produced items, however, have a simplified sealing process, making them prone to fingerprints and oxidation.
Solution
Specify the material grade, unit weight range, and plating and sealing requirements in the order contract. Weigh pre-production samples, and weigh a sample of the bulk order for comparison; conduct material testing if necessary to establish the material specifications.
Functional Differences: Variations in spring tension and the feel of opening and closing
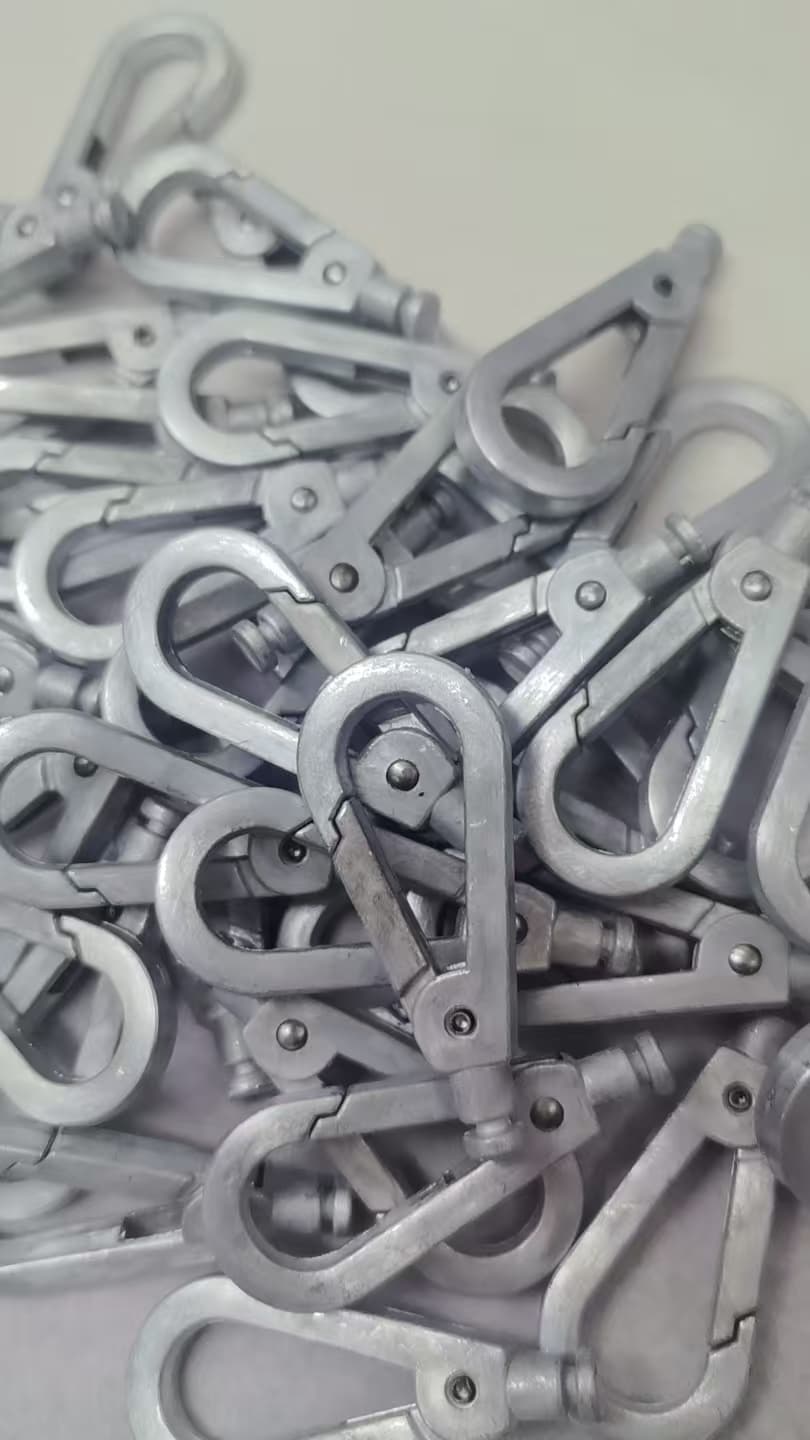
For movable hardware components such as dog clips and snap fasteners, the samples selected are those with the best tactile feel. However, the spring tension in mass-produced items can vary within a certain range. If customers evaluate the product based solely on the feel of the sample without specifying a standard for spring tension, the following issue may arise: the sample opens and closes easily, but the mass-produced items may be too tight or lack sufficient spring return.
Solution
Confirm functionality and feel during the sample stage, and document the spring specifications. For each production batch, conduct random sampling and perform repeated opening and closing tests. Establish an acceptable range, and immediately reject any products that fall outside the specified feel range.
Record target spring‑force range in your order specification sheet instead of only relying on subjective hand‑feel from a single sample.
Standardize Hand‑Over Workflow & Lock Specifications Upfront
Approval samples must be “documented in writing”; verbal commitments are not valid.
Many buyers rely solely on online images for communication and fail to retain sealed, signed samples. When discrepancies arise, both parties end up with conflicting accounts.
Correct Procedure: Prepare two identical copies of the sample, with the client and the hardware manufacturer each retaining one. Both parties should sign and date the samples, noting the order information, material, and plating color. The sample must be clearly marked with the following statement: “This is the sole reference standard for mass production. All subsequent pre-production samples and bulk orders must conform to this physical sample. Photographs are for reference only and cannot be used as a basis for determination.”
Pre‑Production Sample Testing: Critical Step You Cannot Skip
Many customers, in an effort to meet deadlines, skip the pre-production sample stage and proceed directly to mass production—which is the riskiest approach. We produce a pre-production sample using the actual mass-production molds, raw materials, and plating processes, and we use it to verify all specifications in advance.
We can only begin mass production once we have approved the pre-production sample. If we discover a discrepancy with the original sample during the pre-production sample stage, correcting it costs very little; however, if we discover the issue only after we have produced thousands or even tens of thousands of units, the loss is irreparable
Conduct Random Inspections at Each Stage of the Production Process; Don’t Wait Until Shipment to Inspect
Don’t rely solely on a single inspection before shipment for quality control. Conduct random inspections at each stage of the process—die casting, polishing, electroplating, and assembly. Check dimensional accuracy after die casting; check for burrs after polishing; inspect color and plating defects immediately after electroplating; and test functionality after assembly.
Identify issues early and make adjustments promptly to prevent defective products from moving further down the production line.
 | 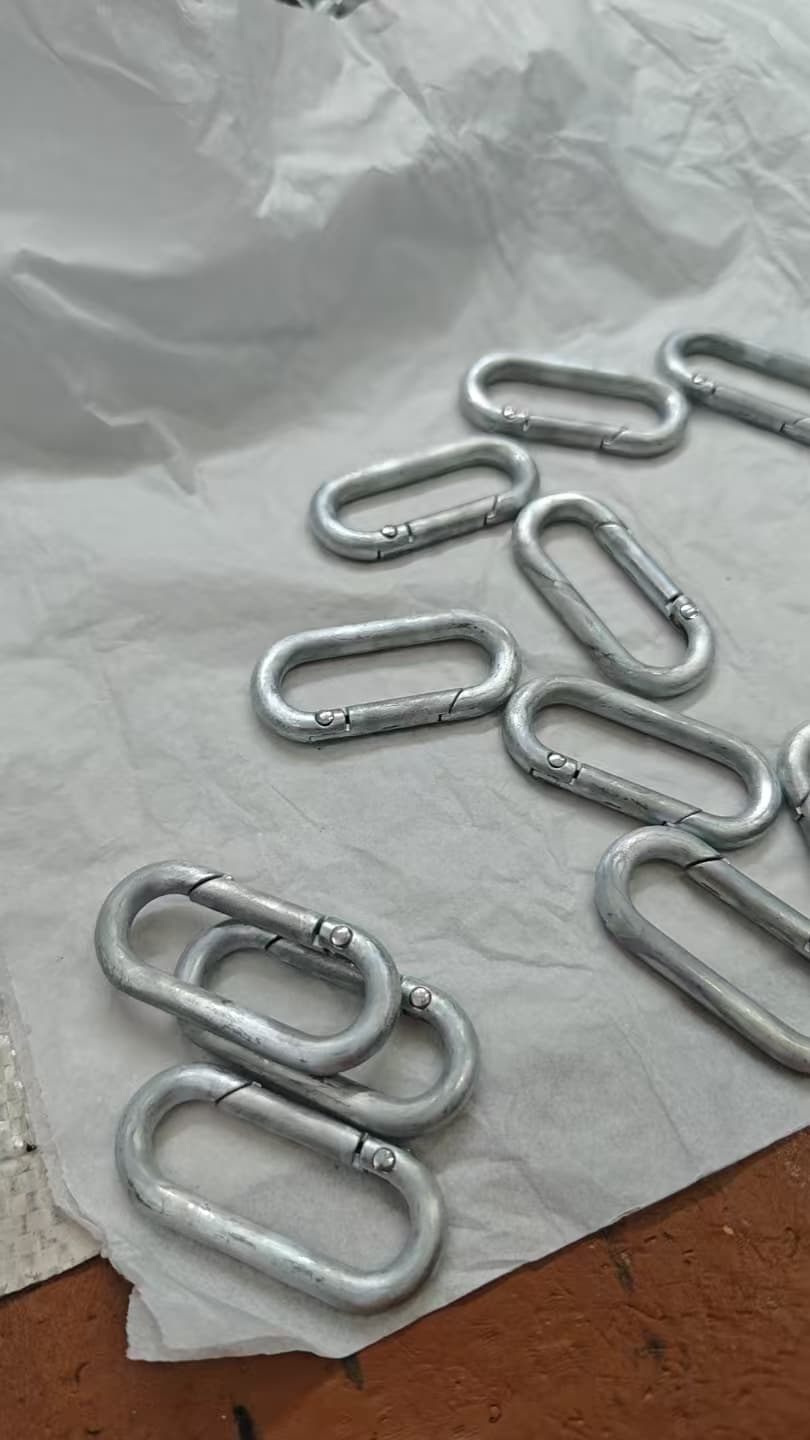 | 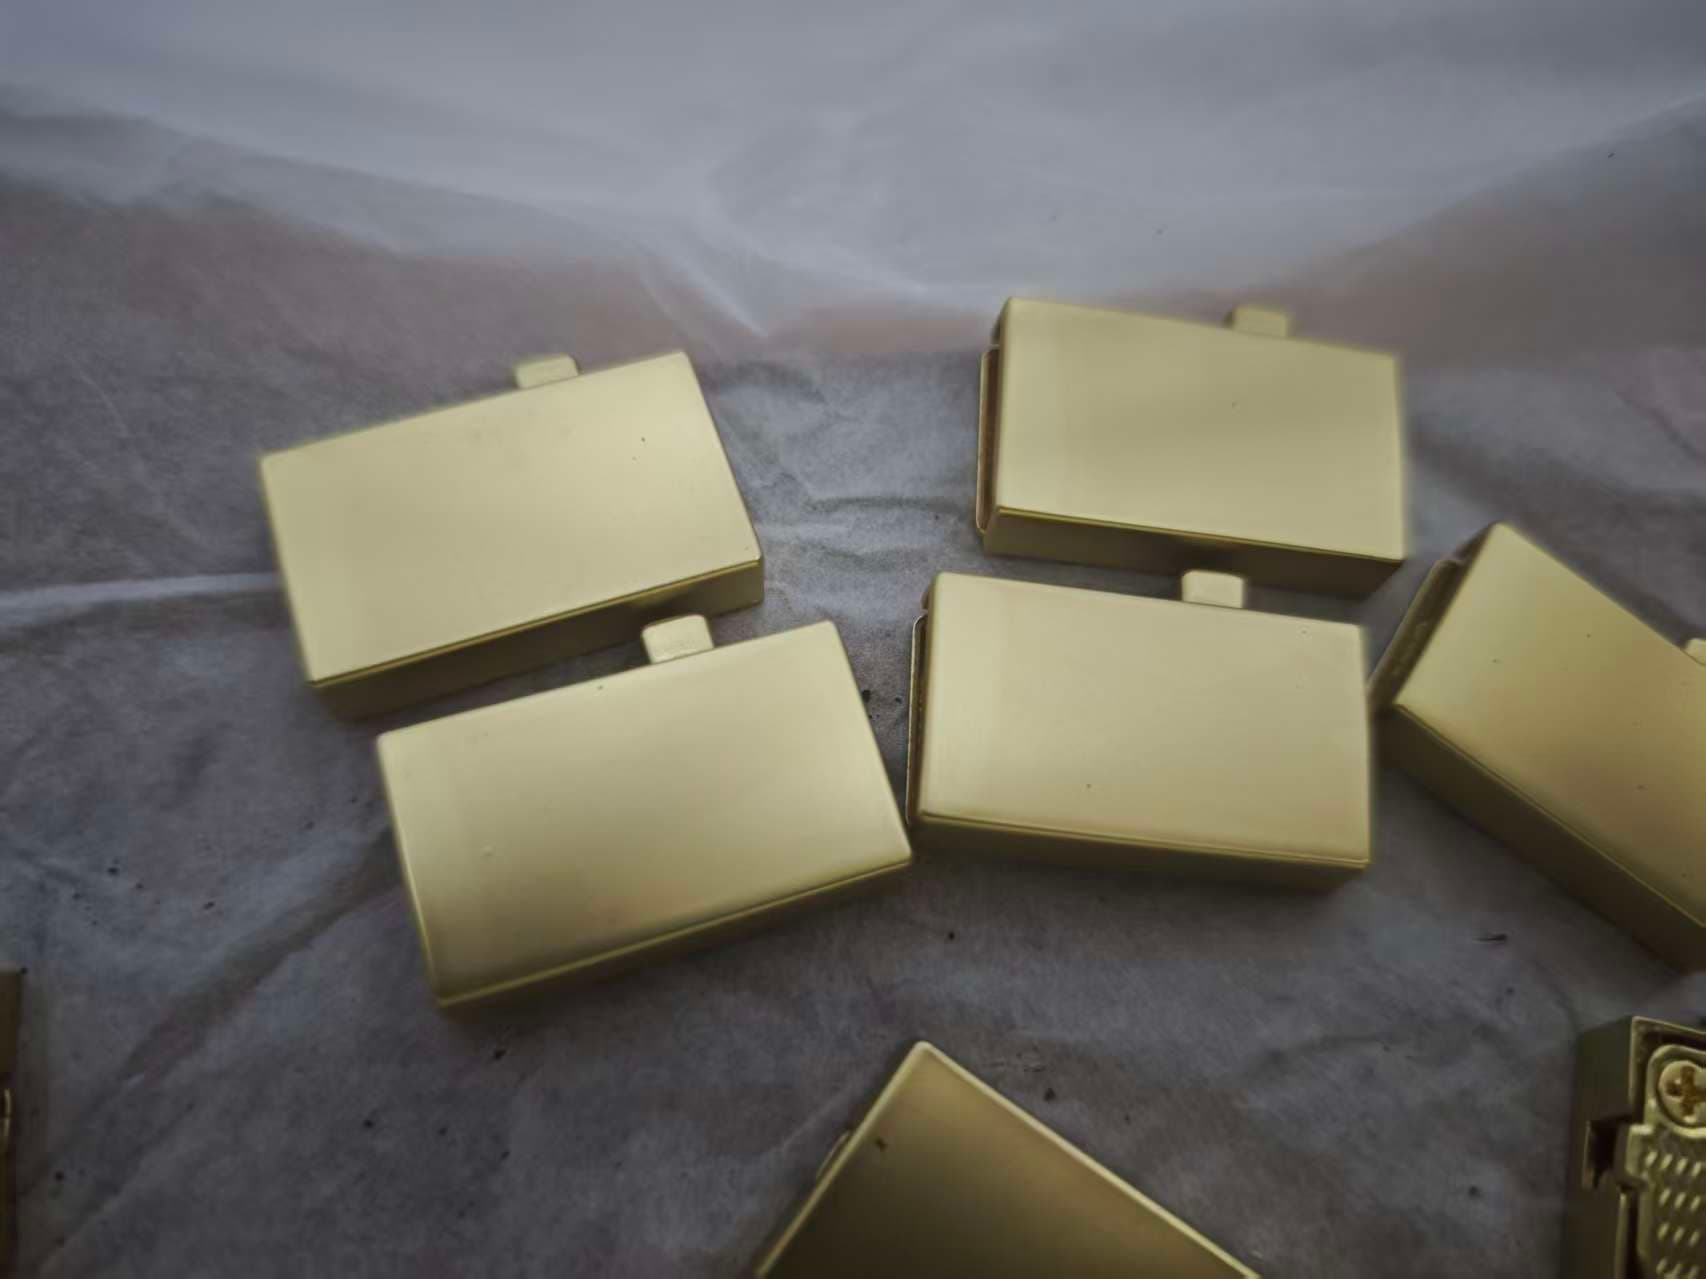 |
| Raw Material Inspection | Post-Assembly Inspection | Finished Product Inspection |
Pre‑Shipment Final Inspection Checklist
Even with in‑process quality control, every batch must be cross‑checked against the sealed reference sample before shipment:
- Dimension check: Measure critical dimensions, thickness and hole positions vs approved sample.
- Functional test: Randomly pick multiple units to test opening‑closing performance and spring rebound feel.
- Visual appearance check: Inspect for scratches, pinholes, burrs following sample acceptance criteria.
- Weight spot‑check: Confirm unit weight matches pre‑production sample to verify material consistency.
Conclusion
Discrepancies between samples and production runs are not inevitable. In many cases, it is not that the factory is intentionally skimping on materials, but rather that there are inherent differences between the sample-making process and the mass production process. To avoid this issue, the key is to materialize the sample standards, insist on pre-production sample approval, conduct quality inspections at each production stage, and perform a final comparison and verification against the signed sample before shipment.
By clearly defining standards in advance and minimizing vague descriptions, both the purchasing department and the supplier can significantly reduce the risk of discrepancies between production runs and samples, minimize rework, claims, and delivery delays, and achieve a stable, long-term partnership.
At OYC Hardware, we strictly follow this full‑set sample‑locking and multi‑stage QC workflow for all custom and stock hardware orders. We provide sealed pre‑production samples before mass run to minimize sample‑bulk deviation for your bag‑manufacturing projects.
Avoid Sample‑Bulk Risks On Your Next Order
📧 [email protected] 📱 WhatsApp: +86-13924451472